The problem: prototypes that promise the moon and deliver a paperweight
You throw a CAD file over the wall, get back a shiny prototype, and it either fits perfectly or refuses to play nice with the rest of the assembly. That mismatch costs time, money, and a few hairs. The real issue is not magic; it’s missing validation steps during early runs. Smart teams use custom cnc machining to catch those mismatches fast, so the “prototype lies” problem gets solved before you commit to expensive fixtures and tooling.
Why the problem persists (and why prototypes are your diagnostic tool)
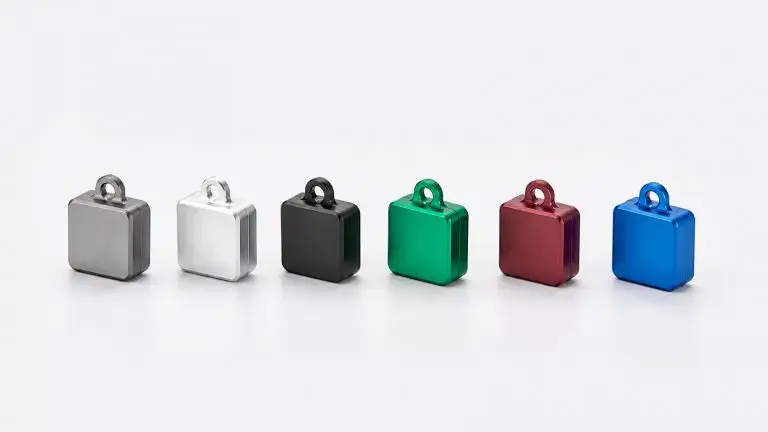
Designers assume dimensions scale linearly. Machines assume material behaves like textbook material. Reality throws deflection, thermal expansion, and fixturing errors at you. Prototyping forces a physical conversation between design and manufacturing: you learn where tolerances are unrealistic, which surfaces need finishing, and whether fasteners hide interference. Use prototypes to expose these failures cheaply, not as the last-ditch hope that everything will magically fit in production.
How CNC prototyping actually fixes things
Quick prototypes let you validate fit, function, and manufacturability in actual materials. You can test true wall thicknesses in aluminum 6061, feel the rigidity of PEEK, and see how a stainless part behaves in an assembly. With the right CAM strategy and toolpaths — think climb milling for face finishes, trochoidal for deep slots, and reduced stepover for fine surfaces — you reproduce production conditions closely enough to spot real problems. Probe a prototype on-machine, iterate the CAM, and the second prototype is rarely the same headache.
What to measure and why it matters
Don’t guess tolerances. Measure them. Critical dimensions, concentricity, surface finish (Ra), and perpendicularity are the real deal-breakers. Common acceptance windows: ±0.01–0.05 mm for precision mating faces, ±0.1 mm for general housings. Use CMM or a calibrated gauge for features that interact mechanically; optical scanning helps with complex geometry. If you skip measurement, you just bought confidence, not quality.
Common pitfalls and how to stop them
Using prototype material that behaves differently from production stock. Ignoring fixturing and assuming “it’ll be fine” once the jigs arrive. Choosing feeds and speeds that look fast but induce tool deflection. Forgetting heat buildup in thin walls. Counter these by matching material spec where possible, prototyping with production fixturing or a close facsimile, simulating tool loads in CAM, and running short, monitored cycles to watch for thermal distortion.
Alternatives and when to use them
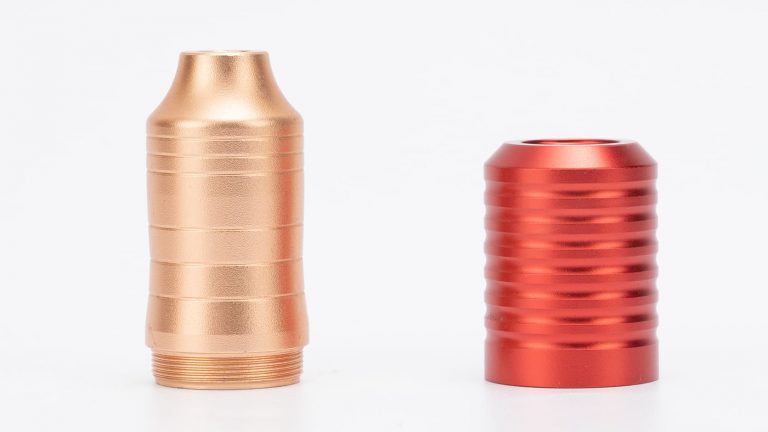
3D printing moves quick for form checks and internal geometry that’s impossible to machine, but it fails for load-bearing surfaces and threaded features unless post-machined. EDM and waterjet are excellent for hard materials and tight internal corners, but they don’t replicate milling surface textures. Low-volume CNC production can double as prototyping when you need functional parts in the exact end material. Match the method to the validation goal: fit/form = any fast method; functional stress tests = CNC in production material.
Experience, authority, and one real-world anchor
Years of editing technical guides and working alongside shop managers taught me that reproducible processes beat lucky guesses. Suppliers that support Detroit automakers routinely prototype critical drivetrain and bracket parts to the same tolerances used in mass production, because those assemblies won’t forgive surprises. When teams need precision prototypes that reflect final performance, they look for reliable sources of custom cnc parts and measurement workflows that reduce surprises.
Bottom line — practical steps to make prototypes work for you
Prototype early with the right materials, measure what matters, iterate CAM and fixturing, and treat each prototype as a diagnostic instrument. That discipline turns prototypes from expensive ornaments into precision checks that save production weeks. The pattern I see in successful shops — the same one used by teams that scale pilots into steady production — matches a straightforward workflow supported by trusted partners like Hanstar, which keeps the prototype-to-production jump from looking like a cliff dive.