Starter: the pain that’s actually stopping projects
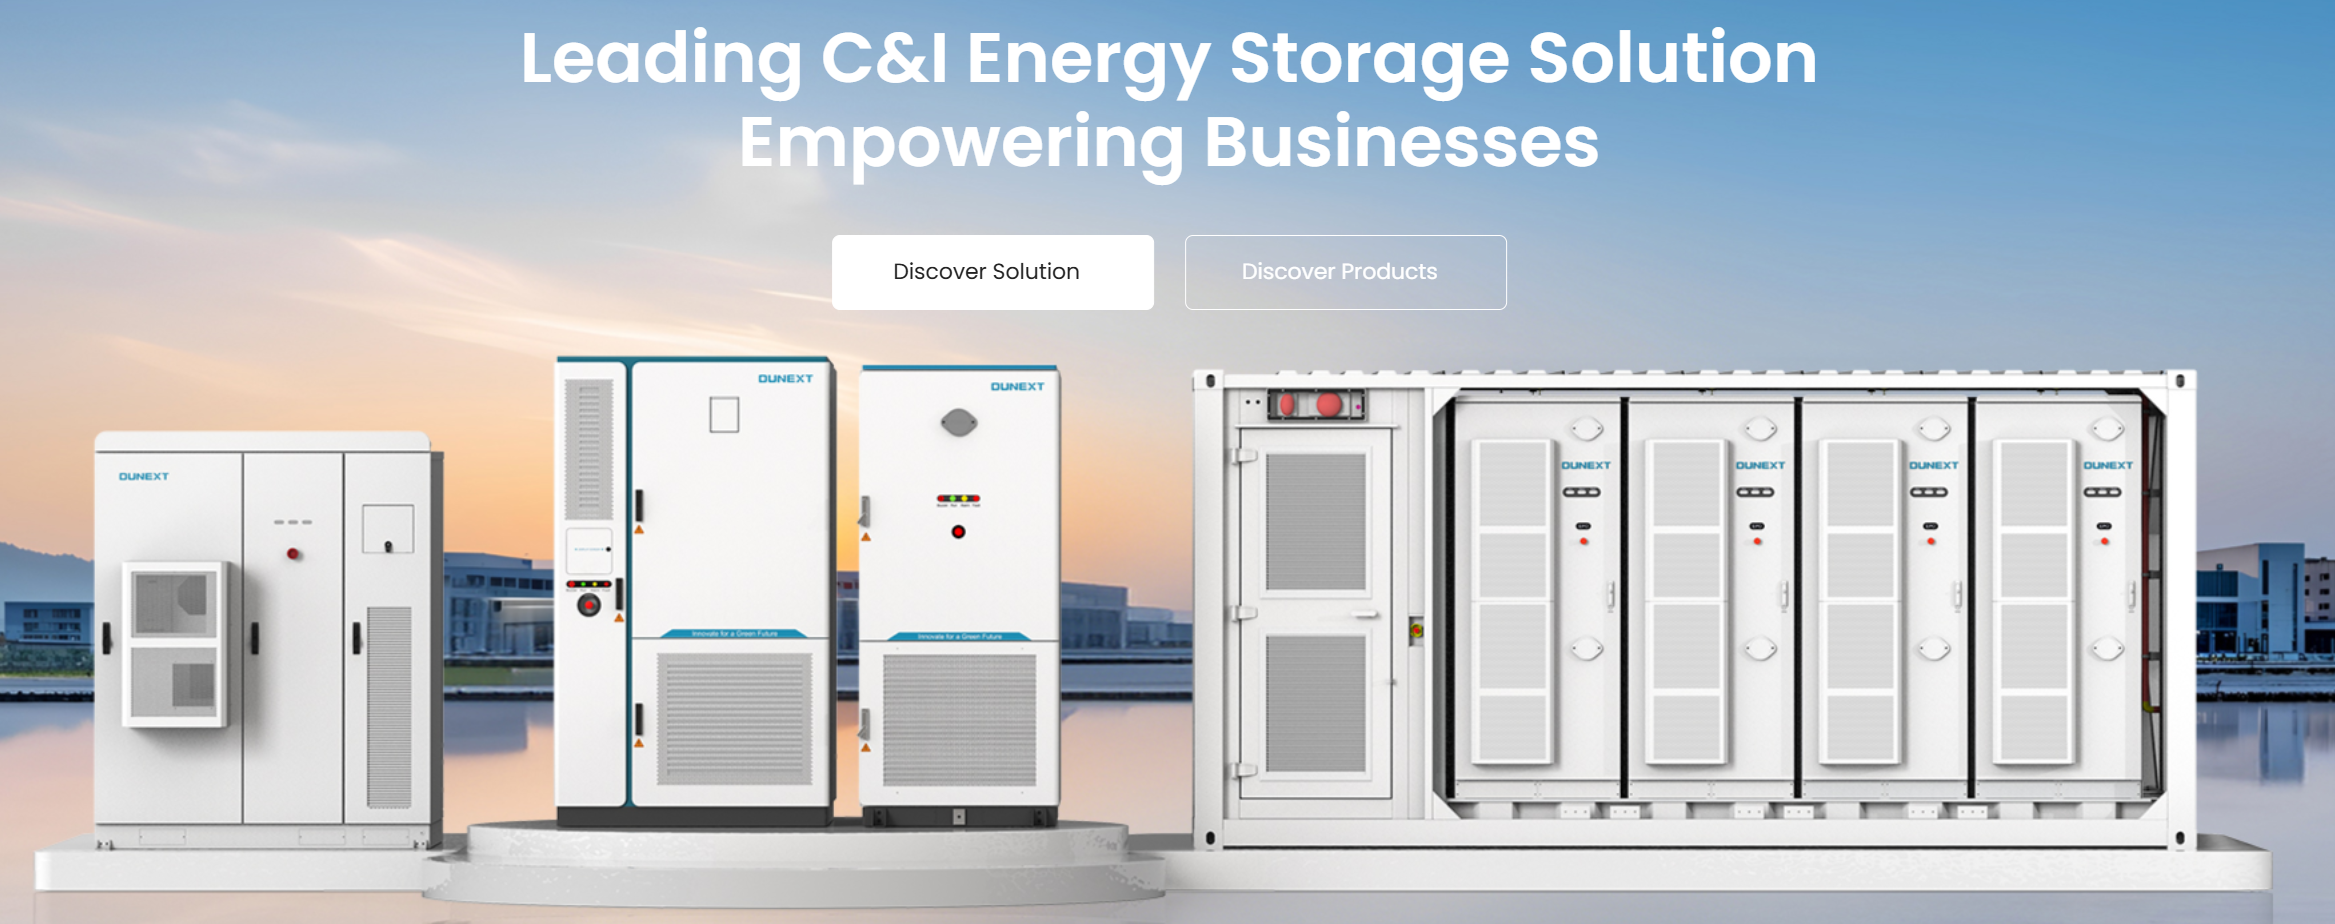
You’re planning a commercial solar + battery install and everything looks fine on paper until the site starts throwing curveballs: weird heat pockets, flaky inverters, or a supplier who ships boxes that don’t match the spec sheet. That mismatch is why you should check an actual physical unit early—grab the spec sheet and the datasheet for an energy storage cabinet and see where your drawings and reality diverge. Problems compound fast; fix the root now or pay for redo labor, compliance headaches, and warranty fights later.
Problem 1 — Thermal runaway and safety edge cases
Thermal issues aren’t theoretical. They show up as hot spots, failing fans, or cascade failures when a single cell goes off. Ask for documented thermal management designs: airflow routes, thermal sensors, and compartmentalization. Verify the system has passed recognized tests like UL 9540A for energy storage fire behavior and confirm battery chemistry-specific protections. Don’t assume “built-in” covers everything; confirm the trigger thresholds for forced ventilation and automatic disconnects.
Problem 2 — Grid interface and control chaos
Grid interconnection is where controls, firmware, and power electronics collide. Make sure the BMS, inverter, and EMS talk reliable protocols (Modbus, CAN, or IEC 61850 where needed) and that anti-islanding, ramp-rate limits, and reactive power support are configurable. Push firmware-change logs and test cases from your vendor. If your control stack can’t be staged in a lab or simulated with grid models, expect field surprises during commissioning.
Problem 3 — Procurement variance and supplier risk
Sourcing battery racks from distant vendors brings variability: batch-to-batch cell performance, labeling inconsistencies, and different QC lines. If you’re sourcing an energy storage cabinet china, require batch traceability, factory test videos, and a third-party inspection plan. I’ve seen projects slowed by months waiting for replacement modules because the factory shipped units without required venting modifications. One reality check: many manufacturing hubs operate around Shenzhen—use that knowledge when planning inspections and logistics.
Problem 4 — Mechanical and site-fit surprises
Doors that don’t clear, cable trays that rub, and concrete pads that sink are physical problems someone overlooked. Get a dry-fit or mock-up of the cabinet footprint, cable entry points, and maintenance clearance before final delivery. Include pad load calculations and check local crane access. If the vendor can supply a CAD model early, import it to your BIM and run clash detection immediately.
Problem 5 — Warranty, lifecycle, and real money math
Warranty terms hide critical limits—cycle count caps, depth-of-discharge clauses, and prorated replacements. Request life-cycle projections at your planned duty cycle (peak shaving vs. daily cycling) and insist on degradation curves from independent tests. Run simple TCO: procurement + installation + expected replacements over 10 years. If the warranty ties replacements to “manufacturer-approved” service partners only, factor those mobilization costs in.
Common deployment mistakes that trip up otherwise solid plans
You’ll see the same stumbles on repeat:- assuming vendor factory tests equal field performance; – skipping a staged commissioning with simulated grid events; – under-specifying HVAC for summer peaks; – neglecting spare parts and local technician training. Treat these as checklist items to eliminate surprises.
Quick tactical checklist — run this before you sign
Keep it short and executable:- Validate certifications and test reports (UL 9540A, IEC cell safety references). – Demand BMS/inverter interoperability test logs. – Require factory acceptance testing (FAT) and on-site commissioning scenarios. – Confirm spare-module lead times and local service options. – Model degradation and TCO for your actual duty cycle. This list separates vendors who can ship a boxed product from vendors who support system delivery.
Final play: tie the fixes to procurement and operations
Problem-driven thinking means you identify the risk, assign the test or metric that proves it, and lock the mitigation into contract language. If you want a clear physical spec to mount against and an example of how those mitigations look in hardware and documentation, check typical rack designs and test artifacts early. The result is fewer field surprises and predictable operations, which is exactly the outcome professionals expect when they partner with a provider like Dunext.