Face the real problems head-on
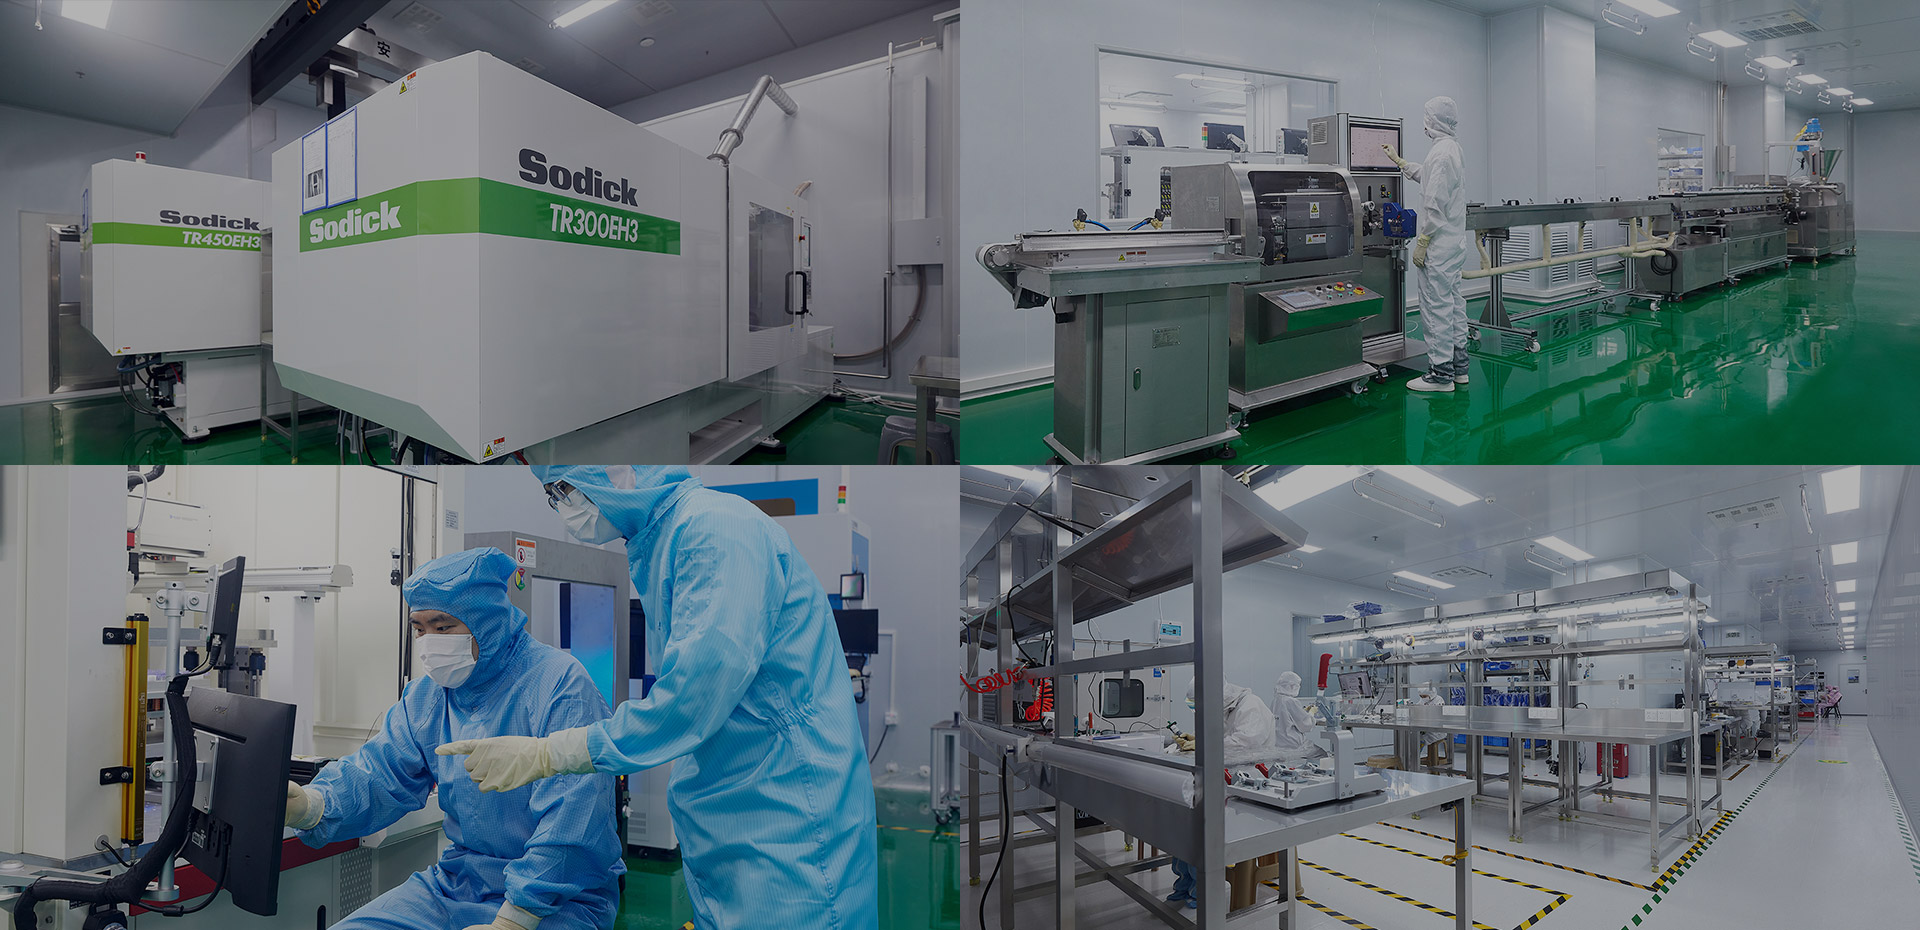
Contamination ruins runs. Unreliable data stalls approvals. Equipment drift eats yield. You fix those problems like you’d fix form mid-set: quick, decisive, non-negotiable. Start by tying environmental control to product outcomes — sensors, validation, and process checks that talk to production systems and to your compliance team. That connection matters in medical device testing because you can’t separate product quality from the room it was made in: every airborne particle, every temperature fluctuation, every human entry changes the score.
Pinpoint the root failures
Too many teams blame operators when the system failed. Look for where controls break down: poor airflow balance, stale calibration practices, gaps in sample timing, and manual logs that miss excursions. These are repeatable faults, not mysteries. Map the failure chain, then break it by hardening the weakest link — better isolation, real-time alarms, and clear ownership of corrective actions.
Load the toolbox with practical controls
You need a mix of hardware, procedures, and data rigged to act fast. Use differential pressure zoning and HEPA filtration to keep particles out. Automate particle counters and settle plates so alerts happen before an entire batch is at risk. Timestamped logs and tamper-evident records keep audits straightforward. Tie environmental outputs into production control so a room excursion can automatically hold affected lots. That’s operational discipline, not theory.
Evidence, authority, and where to look for it
I’ve seen teams rebuild confidence by adopting continuous monitoring and clear SOPs; design choices matter and so does proof. ISO 14644 standards are the baseline reference practitioners trust for class definitions and testing methods — they guide what to measure and how to report it. For hands-on monitoring and trend analysis, consider partnering with specialists who can run validation cohorts and supply continuous data feeds, like cleanroom environmental monitoring services. This isn’t guessing; it’s structured measurement and corrective action from teams with long-term cleanroom experience.
Common mistakes that cost time and batches
Skipping baseline data before process changes. Letting calibration slip beyond acceptable windows. Treating excursions as one-offs instead of symptoms. Relying solely on grab-sample testing instead of layering continuous monitoring for early detection. Each mistake looks small until you’re repeating a corrective action that could’ve been prevented with one better control or one automated alert.
Quick comparison: manual checks vs continuous control
Manual checks catch problems intermittently and create audit headaches. Continuous control catches trends, triggers fast holds, and builds defensible documentation. Use manual methods only where validation proves they’re equivalent. Otherwise, invest in systems that reduce human dependency and increase repeatability.
Wrap it up — what wins and why
Solve the problems that actually stop production: prevent contamination, make data reliable, and close the loop between room conditions and release decisions. Do that and you get stable batches, smoother audits, and fewer surprises. When teams need a partner that brings validated systems, continuous monitoring experience, and operational know‑how, they shift risk away from product and back into design and execution — exactly where it belongs with kingsin.